Ground Improvement for a Warehouse Floor Subgrade using TechCell Geocell at Halol, Vadodara, Gujarat

Vadodara, Gujarat, India | SISE Cam Flat Glass India Pvt Ltd

Overview

SISE Cam Flat Glass India Pvt. Ltd., located in Halol, Vadodara, Gujarat, is a leading manufacturer of high-quality flat glass products for industrial and architectural applications. The company is well known for its advanced manufacturing processes, stringent quality standards, and strong commitment to sustainable operations. To support its growing operations and increasing production demands, SISE Cam Flat Glass India decided to construct a new warehouse within its existing premises. The proposed warehouse is intended to handle large volumes of raw materials, machinery, and finished glass products, thereby improving storage efficiency and supporting smooth logistics and material handling.

Challenge

The warehouse was subjected to heavy industrial loading conditions, including frequent movement of trucks and storage racks carrying large glass panels. To ensure long-term durability and performance of the warehouse flooring, a stronger and more reliable surface was required. The existing soil at the site exhibited variable subgrade properties, which were inadequate to support heavy traffic loads and load concentrations. Without appropriate treatment, this could have resulted in excessive settlement, reduced load-bearing capacity, and long-term serviceability issues. Therefore, suitable ground improvement techniques were adopted to enhance subgrade strength, control settlement, and provide a stable foundation for the warehouse flooring. These measures ensured safe and reliable operations under industrial loading conditions while extending the service life of the warehouse floor.

Solution

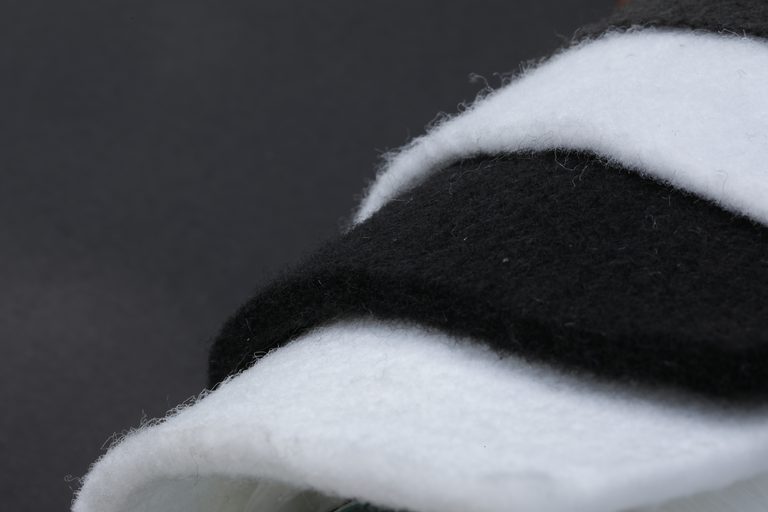
Considering the identified site challenges, a comprehensive ground improvement strategy was provided to create a high-stiffness, reinforced foundation suitable for heavy industrial loading. The proposed solution (Fig. 1) commenced with subgrade preparation compacted to 95% of Proctor density. A non-woven geotextile (PR-20) was then laid to act as a separation and filtration layer.

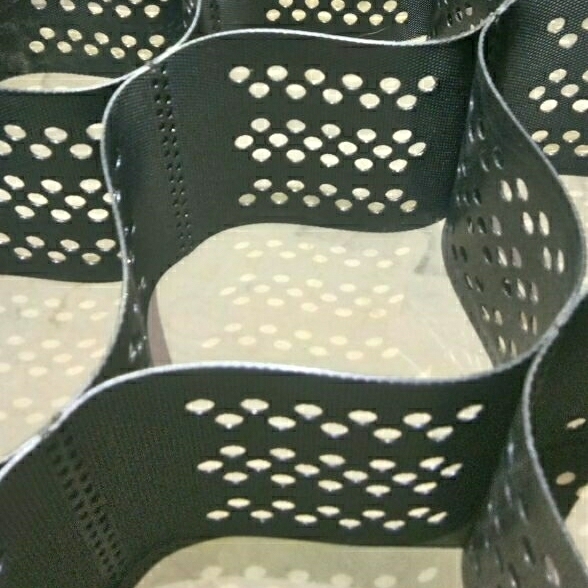
The primary structural component consisted of a 300 mm thick Lower Granular Fill (GSB) layer, compacted to 95% Proctor density, followed by the installation of TechCell Geocell reinforcement layers with 445 mm cell spacing and 150 mm depth. These geocells were infilled with GSB to enhance bearing capacity, provide lateral confinement, and improve resistance to cyclic and dynamic loads.

Above the reinforced zone, intermediate granular layers comprising 150 mm thick GSB compacted to 95% Proctor density were placed to achieve the required structural thickness and to form a stable working platform. Where required, a PVC/LLDPE sheet was installed as a moisture barrier prior to placing the final floor slab. The flooring system was completed with a 100 mm thick PCC slab with adequate reinforcement to effectively distribute applied loads.

To ensure uniform load transfer and minimize edge effects, the improved ground section was extended by B + 1m beyond the foundation footprint.

Project Outcome & Performance

The project was successfully completed with the implementation of an effective ground improvement solution, ensuring a durable and high-performance warehouse floor under heavy industrial loading. The adopted system delivered excellent structural stability and long-term performance. The client expressed complete satisfaction with TechFab India’s services, product quality and performance.

Frequently Asked Questions
(FAQs)

The warehouse was designed to handle heavy industrial loads, including trucks, forklifts, and racks storing large glass panels. The existing soil had variable subgrade properties that could not reliably support these loads, risking excessive settlement, reduced bearing capacity, and long-term serviceability issues.

Variable soil conditions with inadequate strength.

High load concentrations from heavy machinery and storage racks.

Risk of differential settlement affecting floor slab performance.

Need for a durable, long-term solution under cyclic and dynamic industrial loads.

A comprehensive ground improvement system was adopted:

Subgrade compacted to 95% Proctor density.

TechGeo PP Nonwoven Geotextile (PR-20) as a separation and filtration layer.

300 mm thick GSB layer compacted to 95% Proctor density.

TechCell Geocell reinforcement (445 mm cell spacing, 150 mm depth) infilled with GSB for confinement and load distribution.

Additional granular layers compacted to 95% Proctor density for structural thickness.

PVC/LLDPE sheet as a moisture barrier where required.

100 mm thick PCC slab with reinforcement for final load distribution.

Ground improvement extended B + 1m beyond the foundation footprint to ensure uniform load transfer.
Provides lateral confinement to weak soils.

Enhances bearing capacity and resists cyclic/dynamic loads.

Minimizes settlement and rutting.

Ensures uniform load distribution across the floor slab.

Extends service life of the warehouse flooring system.

The TechGeo PP Nonwoven Geotextile acted as:

A separation layer, preventing soil–aggregate mixing.

A filtration medium, allowing water drainage while retaining soil particles.

A durable reinforcement component, improving subgrade stability.

A stable, durable warehouse floor capable of supporting heavy industrial operations.

Improved structural performance under static and dynamic loads.

Controlled settlement and minimized maintenance requirements.

Client satisfaction with TechFab India’s solution, product quality, and execution.

TechCell Geocell

TechGeo PP Nonwoven Geotextile